Introduction
The manufacturing landscape is undergoing a transformative shift driven by the convergence of digital technologies, automation, and data-driven decision-making. This evolution, often referred to as Industry 4.0, represents the fourth industrial revolution, characterized by the integration of cyber-physical systems, the Internet of Things (IoT), artificial intelligence (AI), and advanced analytics. Unlike its predecessors, which focused on mechanization, electricity, and computerization, Industry 4.0 emphasizes interconnectedness, real-time data, and intelligent automation. This article explores the core components, opportunities, challenges, and future potential of Industry 4.0, offering a fresh perspective on its impact on global manufacturing.
The Pillars of Industry 4.0
Industry 4.0 is built on several technological pillars that enable smarter, more efficient, and more flexible production processes. These include:
Cyber-Physical Systems (CPS)
Cyber-physical systems integrate physical machinery with digital systems, creating a seamless interaction between the physical and virtual worlds. In a smart factory, CPS enables machines to communicate with each other, monitor processes, and make autonomous decisions. For example, a robotic arm equipped with sensors can adjust its movements based on real-time feedback, reducing errors and improving efficiency.
Internet of Things (IoT)
The IoT connects devices, sensors, and machines across the production floor, enabling real-time data collection and sharing. IoT devices monitor equipment health, track inventory, and optimize supply chains. For instance, IoT-enabled sensors in a warehouse can detect low stock levels and automatically trigger reordering, minimizing downtime.
Artificial Intelligence and Machine Learning
AI and machine learning (ML) empower manufacturers to analyze vast datasets, predict outcomes, and optimize operations. Predictive maintenance, powered by AI, uses historical and real-time data to forecast equipment failures before they occur, reducing costly downtime. Additionally, ML algorithms can optimize production schedules by analyzing demand patterns and resource availability.
Big Data and Analytics
The volume of data generated in modern manufacturing is staggering. Big data analytics processes this information to uncover insights, identify inefficiencies, and drive decision-making. For example, analyzing production data can reveal bottlenecks in the assembly line, enabling targeted improvements.
Cloud Computing
Cloud computing provides scalable storage and processing power, allowing manufacturers to access data and applications from anywhere. It supports real-time collaboration across global supply chains and enables small and medium-sized enterprises (SMEs) to adopt Industry 4.0 technologies without significant upfront investments.
Additive Manufacturing
Also known as 3D printing, additive manufacturing allows for rapid prototyping and the production of complex parts with minimal waste. It enables customization at scale, which is particularly valuable in industries like aerospace and healthcare.
Augmented Reality (AR) and Virtual Reality (VR)
AR and VR enhance training, maintenance, and design processes. Technicians can use AR glasses to access real-time instructions while repairing equipment, while VR simulations allow engineers to test factory layouts virtually before implementation.
The Impact of Industry 4.0 on Manufacturing
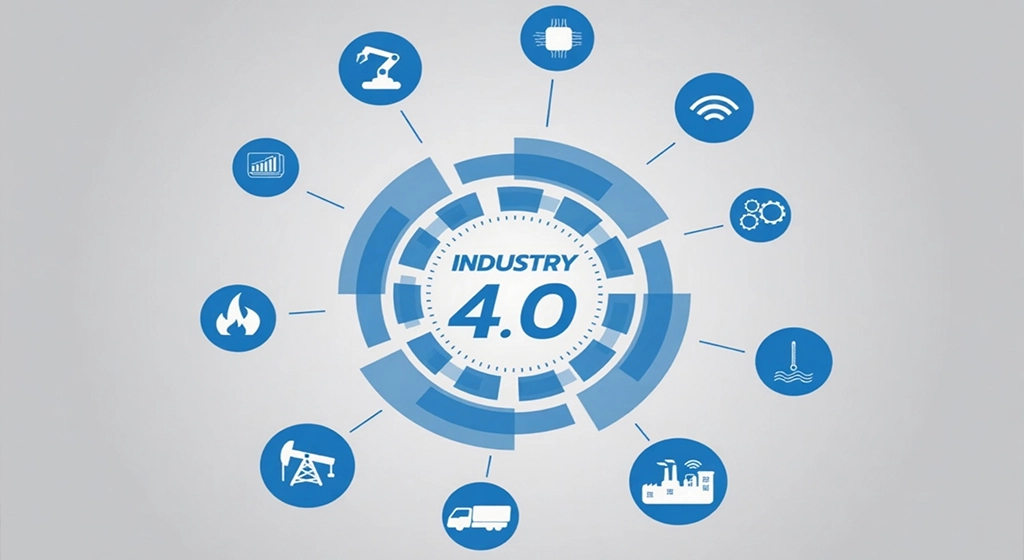
Industry 4.0 is reshaping manufacturing in profound ways, offering benefits that enhance productivity, sustainability, and competitiveness.
Enhanced Productivity
Smart factories leverage automation and real-time data to streamline operations. For instance, IoT-enabled machines can self-optimize, reducing cycle times and increasing output. A 2023 study by the World Economic Forum estimated that Industry 4.0 technologies could boost global manufacturing productivity by up to 30% by 2030.
Customization and Flexibility
Industry 4.0 enables mass customization, allowing manufacturers to produce tailored products without sacrificing efficiency. For example, automotive manufacturers can use flexible production lines to switch between different vehicle models seamlessly, meeting diverse customer demands.
Sustainability
By optimizing resource use and reducing waste, Industry 4.0 supports sustainable manufacturing. Energy-efficient machines, predictive maintenance, and additive manufacturing minimize environmental impact. A European Union report highlighted that smart factories could reduce energy consumption in manufacturing by up to 20% by 2035.
Supply Chain Resilience
Interconnected systems improve supply chain transparency and agility. IoT and blockchain technologies enable real-time tracking of goods, reducing delays and ensuring traceability. During disruptions, such as the 2020 pandemic, companies with Industry 4.0-enabled supply chains were better equipped to adapt.
Challenges in Adopting Industry 4.0
Despite its potential, Industry 4.0 adoption faces several hurdles that must be addressed to ensure widespread success.
High Initial Costs
Implementing Industry 4.0 technologies requires significant investment in infrastructure, software, and workforce training. SMEs, in particular, may struggle to afford these upfront costs, creating a digital divide between large corporations and smaller players.
Cybersecurity Risks
The interconnected nature of Industry 4.0 increases vulnerability to cyberattacks. A single breach in a smart factory could compromise sensitive data or halt production. Manufacturers must invest in robust cybersecurity measures, such as encryption and intrusion detection systems, to mitigate these risks.
Workforce Transition
The shift to smart manufacturing demands a workforce skilled in digital technologies. However, many workers lack the necessary training in AI, data analytics, or IoT. Upskilling programs and partnerships with educational institutions are critical to bridging this skills gap.
Data Overload
The sheer volume of data generated by Industry 4.0 systems can overwhelm organizations. Without effective data management strategies, manufacturers may struggle to extract meaningful insights, leading to inefficiencies.
Interoperability Issues
Integrating legacy systems with new technologies can be challenging. Many factories rely on outdated equipment that is incompatible with modern IoT or AI solutions. Standardization and modular systems are needed to ensure seamless integration.
Industry 4.0 in Action: Real-World Examples
Several industries are already leveraging Industry 4.0 to drive innovation and efficiency.
Automotive Industry
Leading automakers, such as BMW and Tesla, have embraced smart factories. BMW’s Dingolfing plant in Germany uses IoT and AI to optimize production, with robots and humans collaborating on flexible assembly lines. This has reduced production times by 15% while enabling greater customization.
Healthcare
In healthcare, additive manufacturing is revolutionizing the production of medical devices. Companies like Stryker use 3D printing to create patient-specific implants, improving outcomes and reducing costs. IoT-enabled devices also monitor patient health remotely, integrating data into hospital systems.
Consumer Goods
Procter & Gamble employs digital twins—virtual replicas of physical assets—to simulate and optimize production processes. By testing changes virtually, the company reduces downtime and improves product quality.
The Role of SMEs in Industry 4.0
While large corporations often lead the charge, SMEs play a crucial role in the Industry 4.0 ecosystem. Cloud-based solutions and affordable IoT devices have lowered the barrier to entry, enabling smaller firms to adopt smart technologies. For example, a small textile manufacturer in India implemented IoT sensors to monitor machinery, reducing maintenance costs by 25%. Governments and industry associations can further support SMEs through subsidies, training programs, and access to shared innovation hubs.
The Future of Industry 4.0
As Industry 4.0 matures, several trends are shaping its future trajectory.
AI-Driven Autonomy
Advancements in AI will enable fully autonomous factories, where machines make real-time decisions without human intervention. This could lead to “lights-out” manufacturing, where production continues 24/7 with minimal oversight.
Human-Machine Collaboration
Rather than replacing workers, Industry 4.0 will foster closer collaboration between humans and machines. Cobots (collaborative robots) will work alongside employees, enhancing productivity and safety.
Circular Economy
Industry 4.0 technologies will drive the transition to a circular economy by enabling recycling, reusing, and repurposing materials. For instance, IoT and blockchain can track product lifecycles, ensuring sustainable disposal and reuse.
Edge Computing
Edge computing, which processes data closer to its source, will reduce latency and improve real-time decision-making in smart factories. This is particularly valuable for applications requiring instant responses, such as autonomous robots.
Global Collaboration
As supply chains become more interconnected, Industry 4.0 will facilitate global collaboration. Digital platforms will enable manufacturers, suppliers, and customers to share data seamlessly, fostering innovation and efficiency.
Ethical and Societal Considerations
The widespread adoption of Industry 4.0 raises important ethical questions. Automation may lead to job displacement in certain sectors, necessitating robust reskilling programs. Additionally, the reliance on data-driven systems raises concerns about privacy and data ownership. Manufacturers must prioritize transparency and ethical data practices to maintain public trust.
Conclusion
Industry 4.0 is not merely a technological upgrade but a paradigm shift that redefines manufacturing. By integrating cyber-physical systems, IoT, AI, and other technologies, it unlocks unprecedented opportunities for efficiency, customization, and sustainability. However, challenges such as high costs, cybersecurity risks, and workforce transitions must be addressed to ensure equitable access. As we look to the future, Industry 4.0 promises to create a more connected, intelligent, and sustainable manufacturing ecosystem, paving the way for a new era of industrial innovation.



